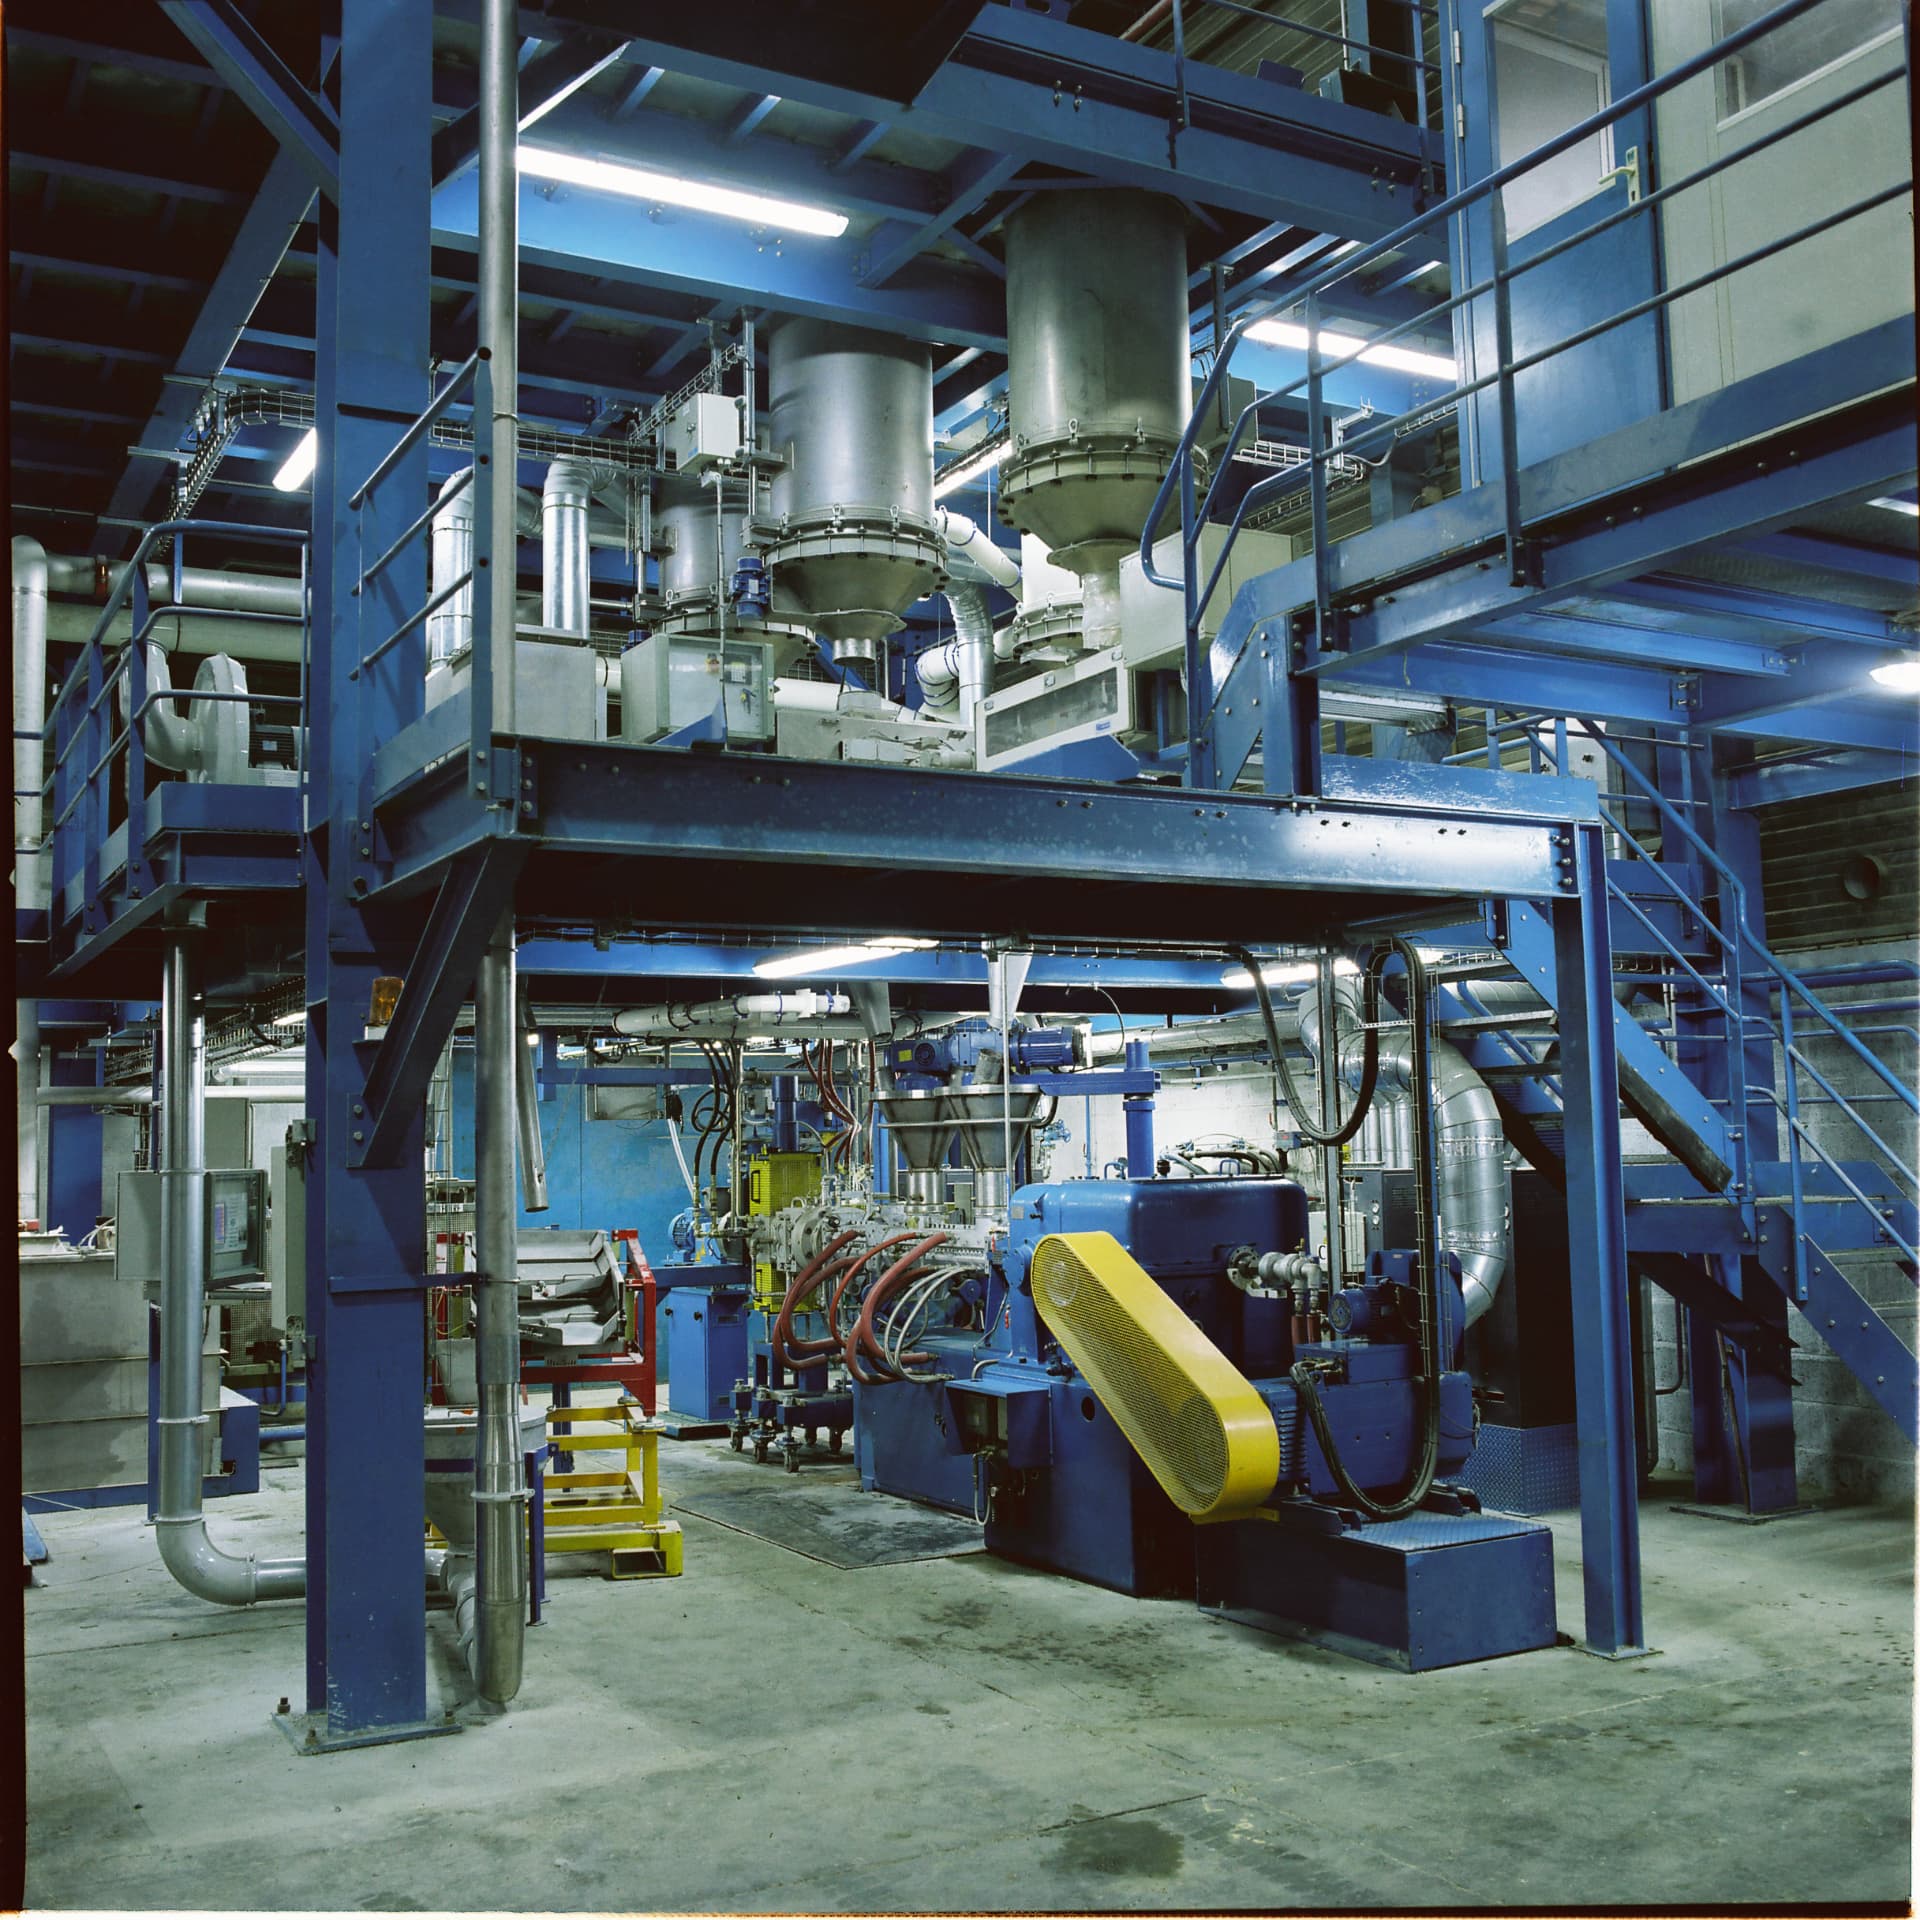
BUSS co-kneaders
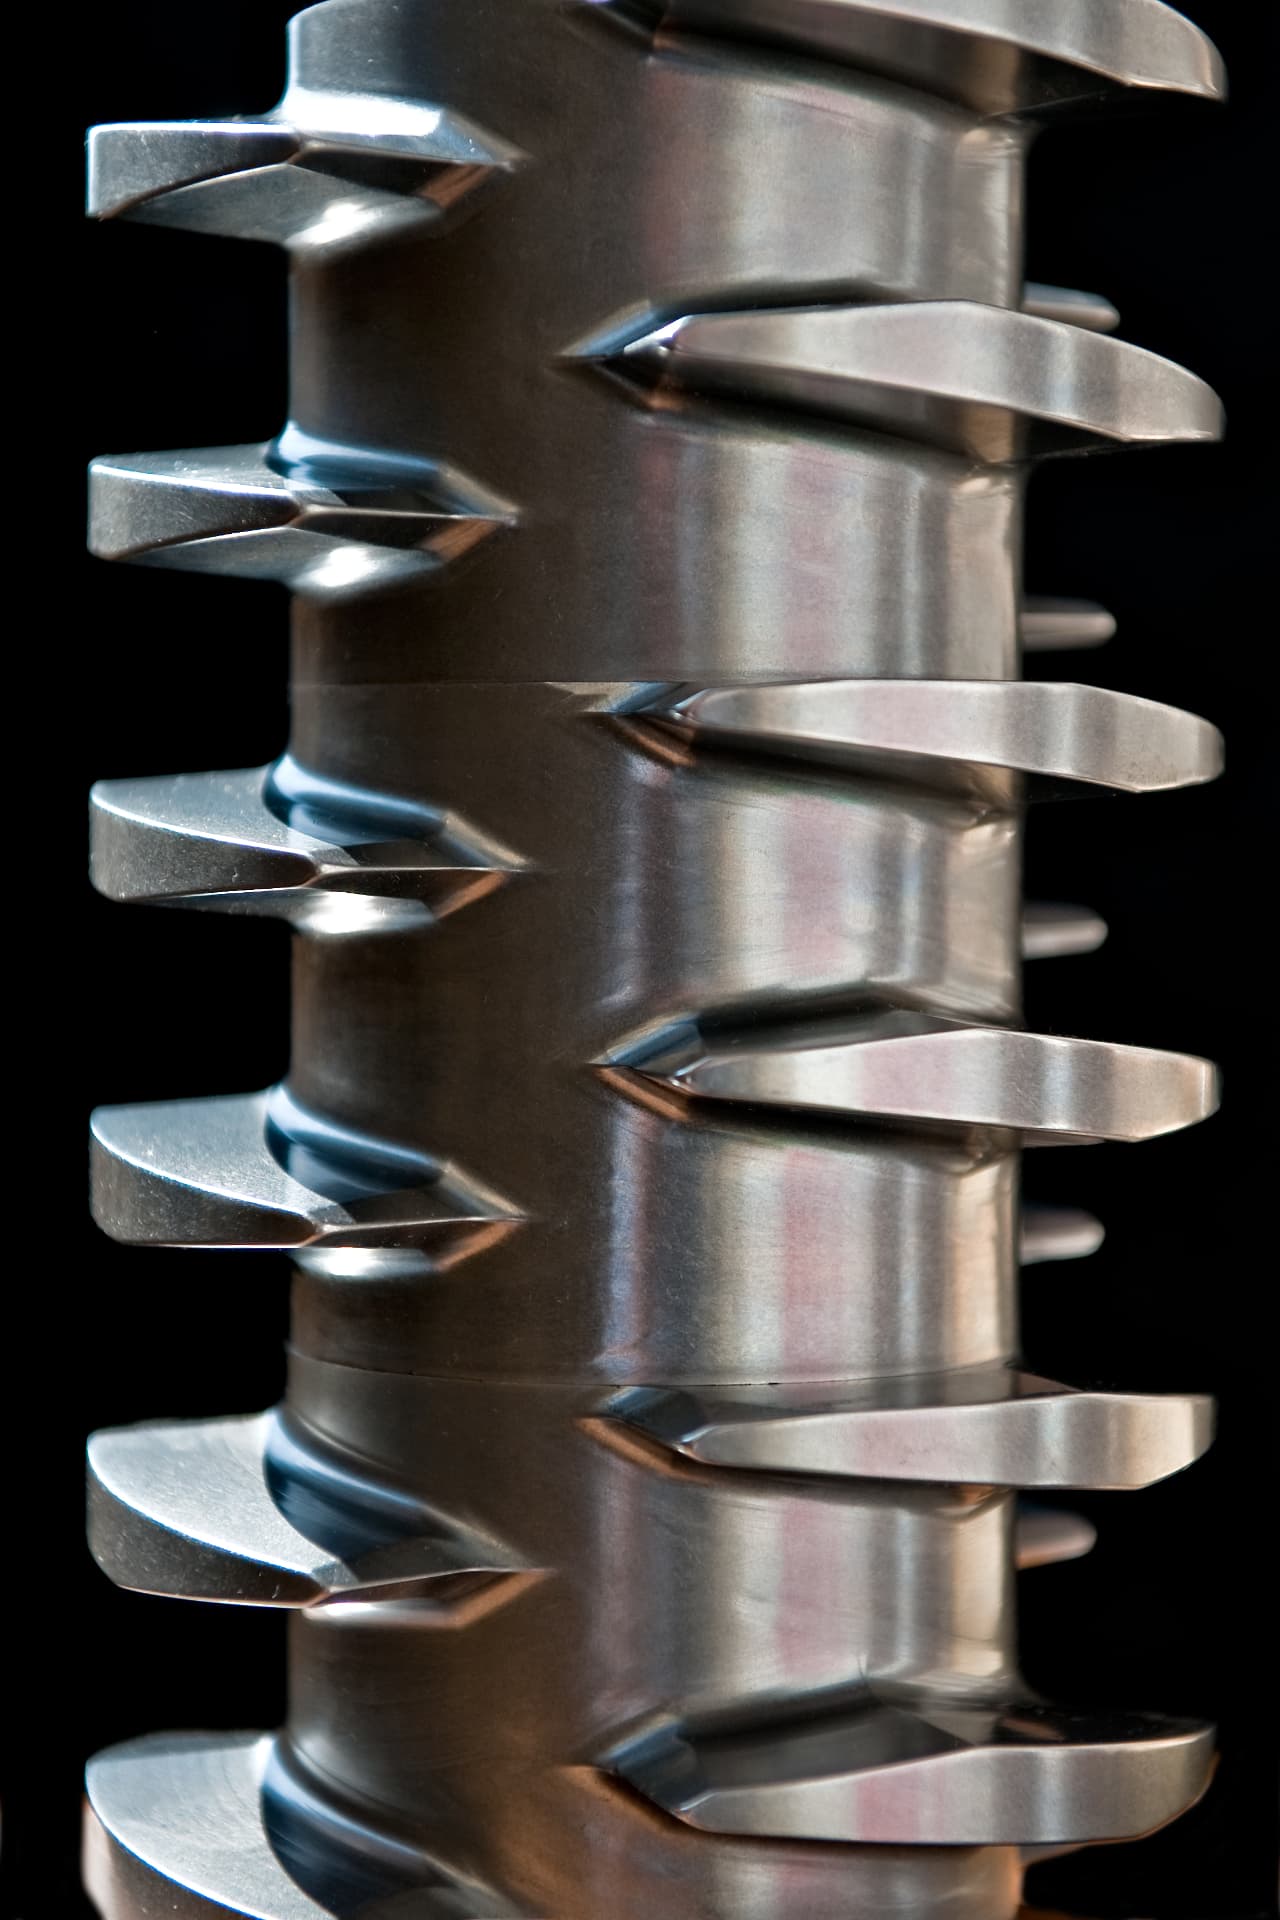
Low, even shear and tight temperature control for heat-sensitive and highly filled compounds, including HFFR cable grades.
 — home
Polytolling® · Specialty toll compounding · Since 1980
The compounding step you were missing.
BUSS co-kneaders, twin-screw reactive extrusion, viscous liquid injection and non-dusting blends across 18+ lines in Normandy. We run your recipe under NDA, from lab trial to production campaigns, on the same line configuration and with the same team.
The specialty compounder you call when standard extrusion isn't enough.
Companies come to us for one of three reasons: their lines are full, they need a second source, or they want to test a formulation without investing first.
Deglobalisation and import barriers make an EU production base more valuable every year, and grid electrification is pushing HFFR cable-compound demand beyond many producers' in-house capacity. Our AEO customs status keeps cross-border flows simple.
Our machines and process know-how are combined around each formulation.
Low, even shear and tight temperature control for heat-sensitive and highly filled compounds, including HFFR cable grades.
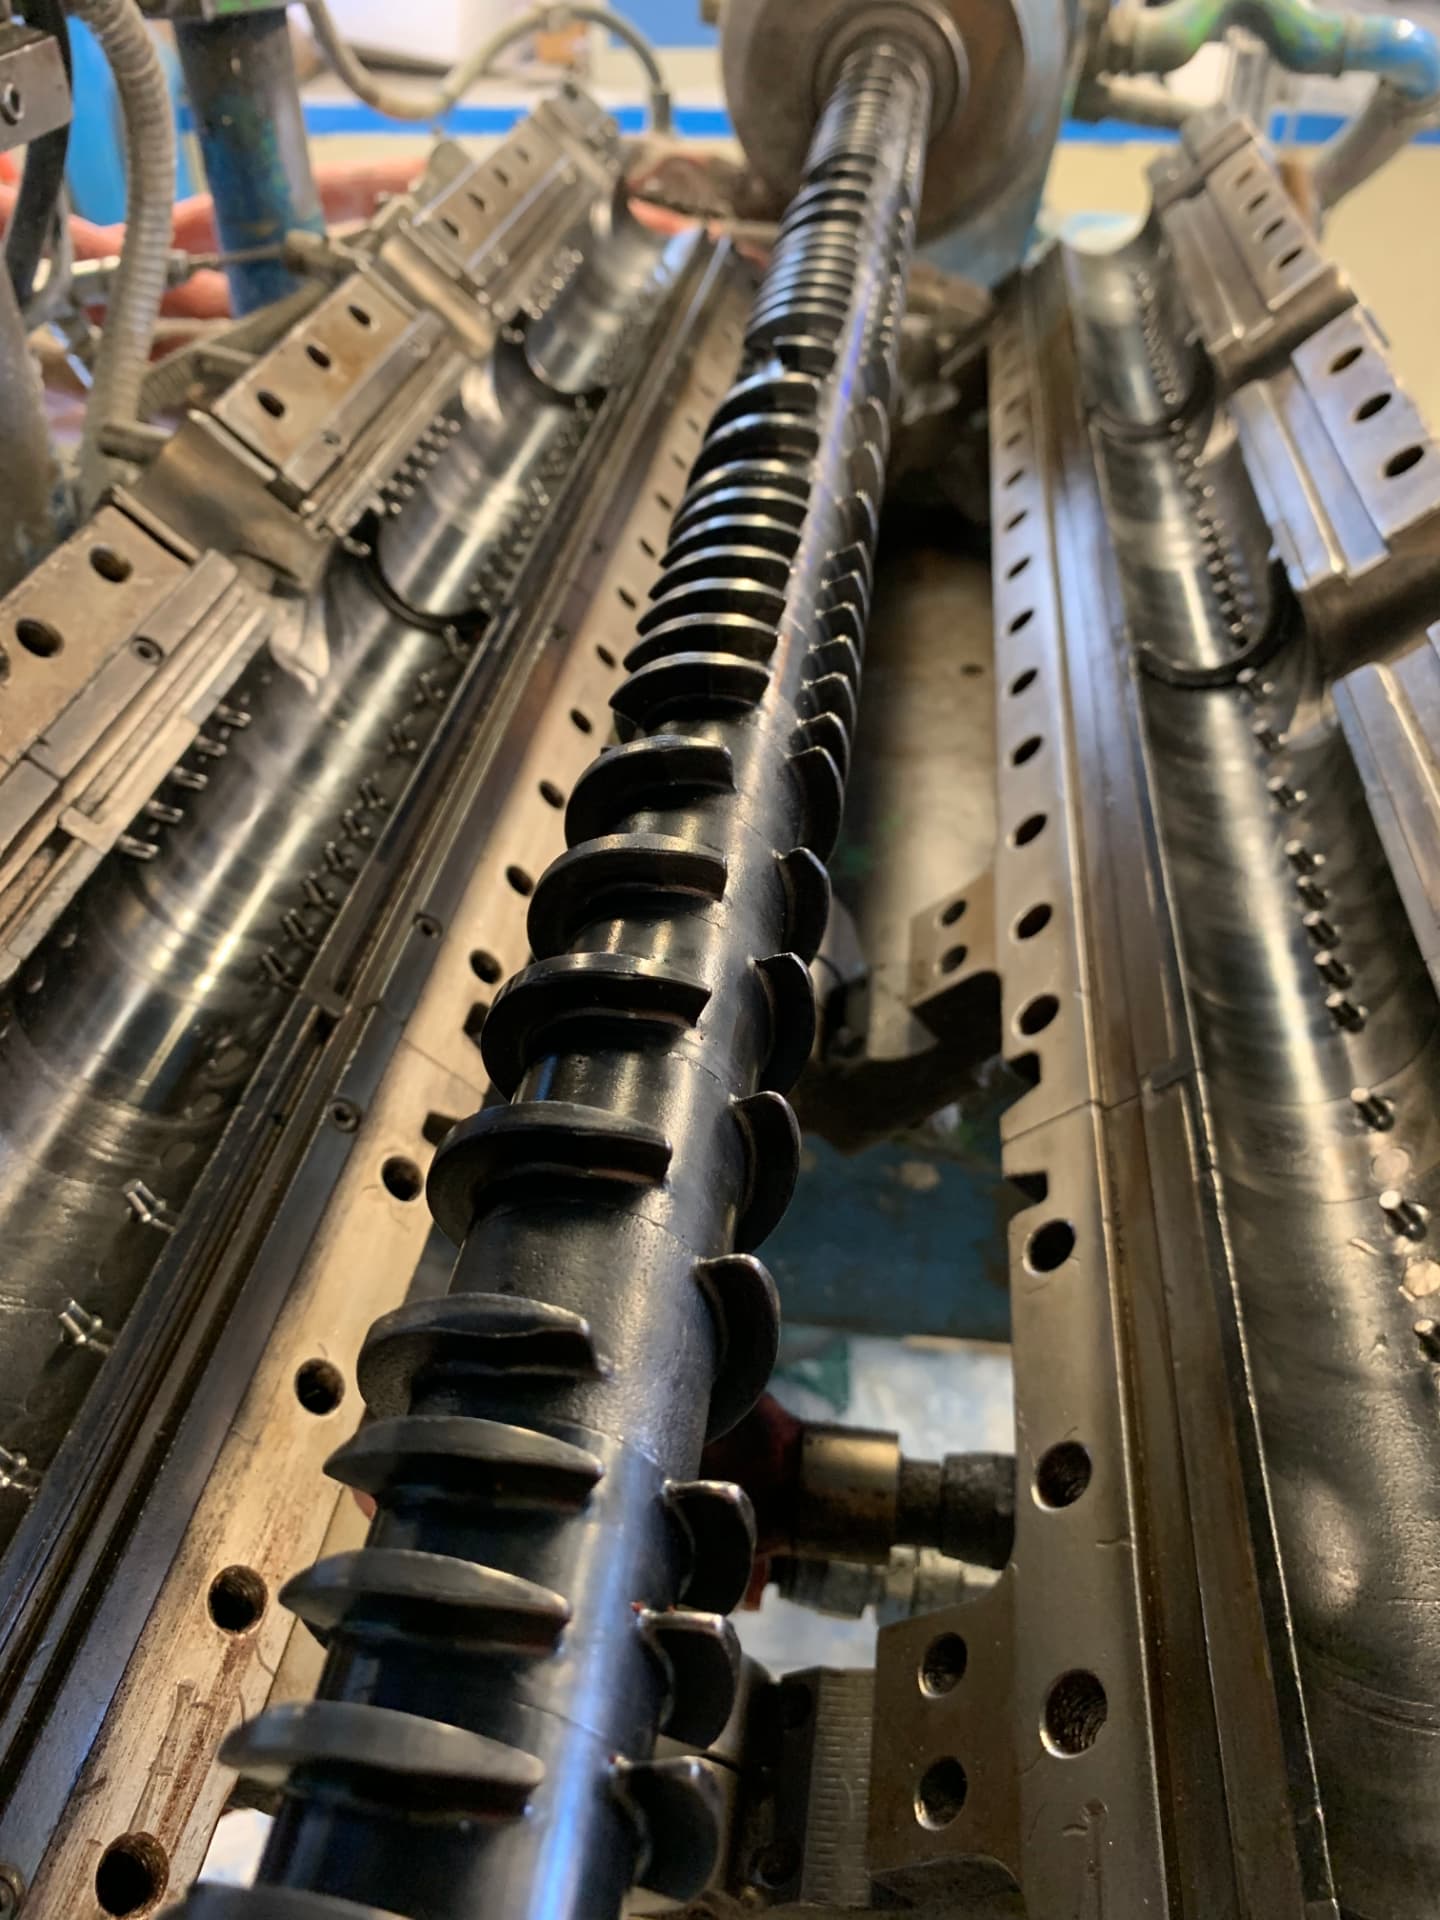
Reactive extrusion, phase transfer, devolatilisation and high-loading liquid injection.
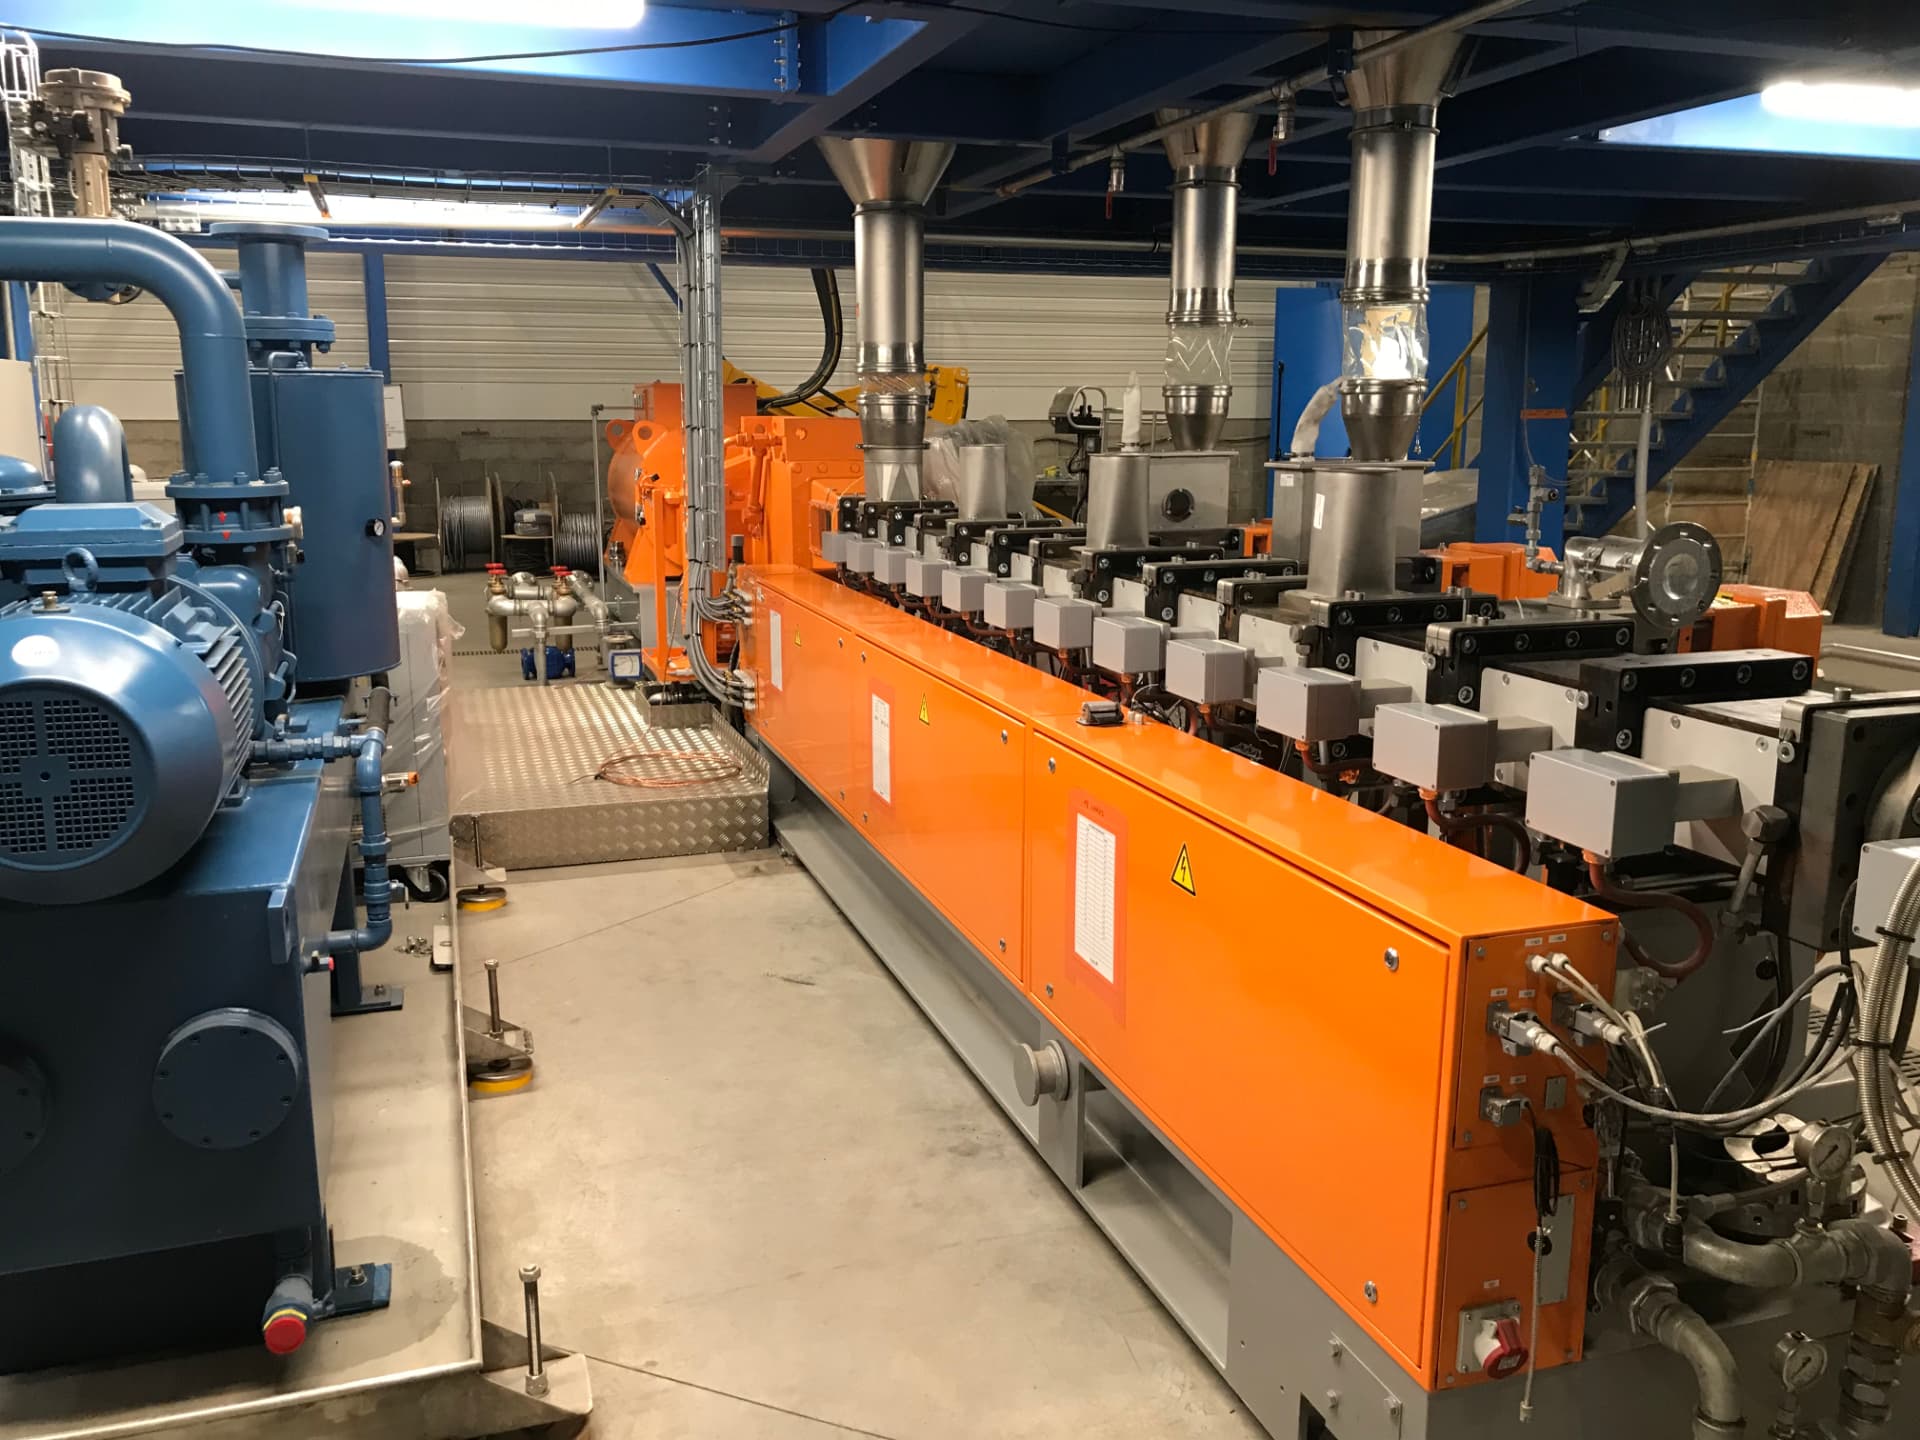
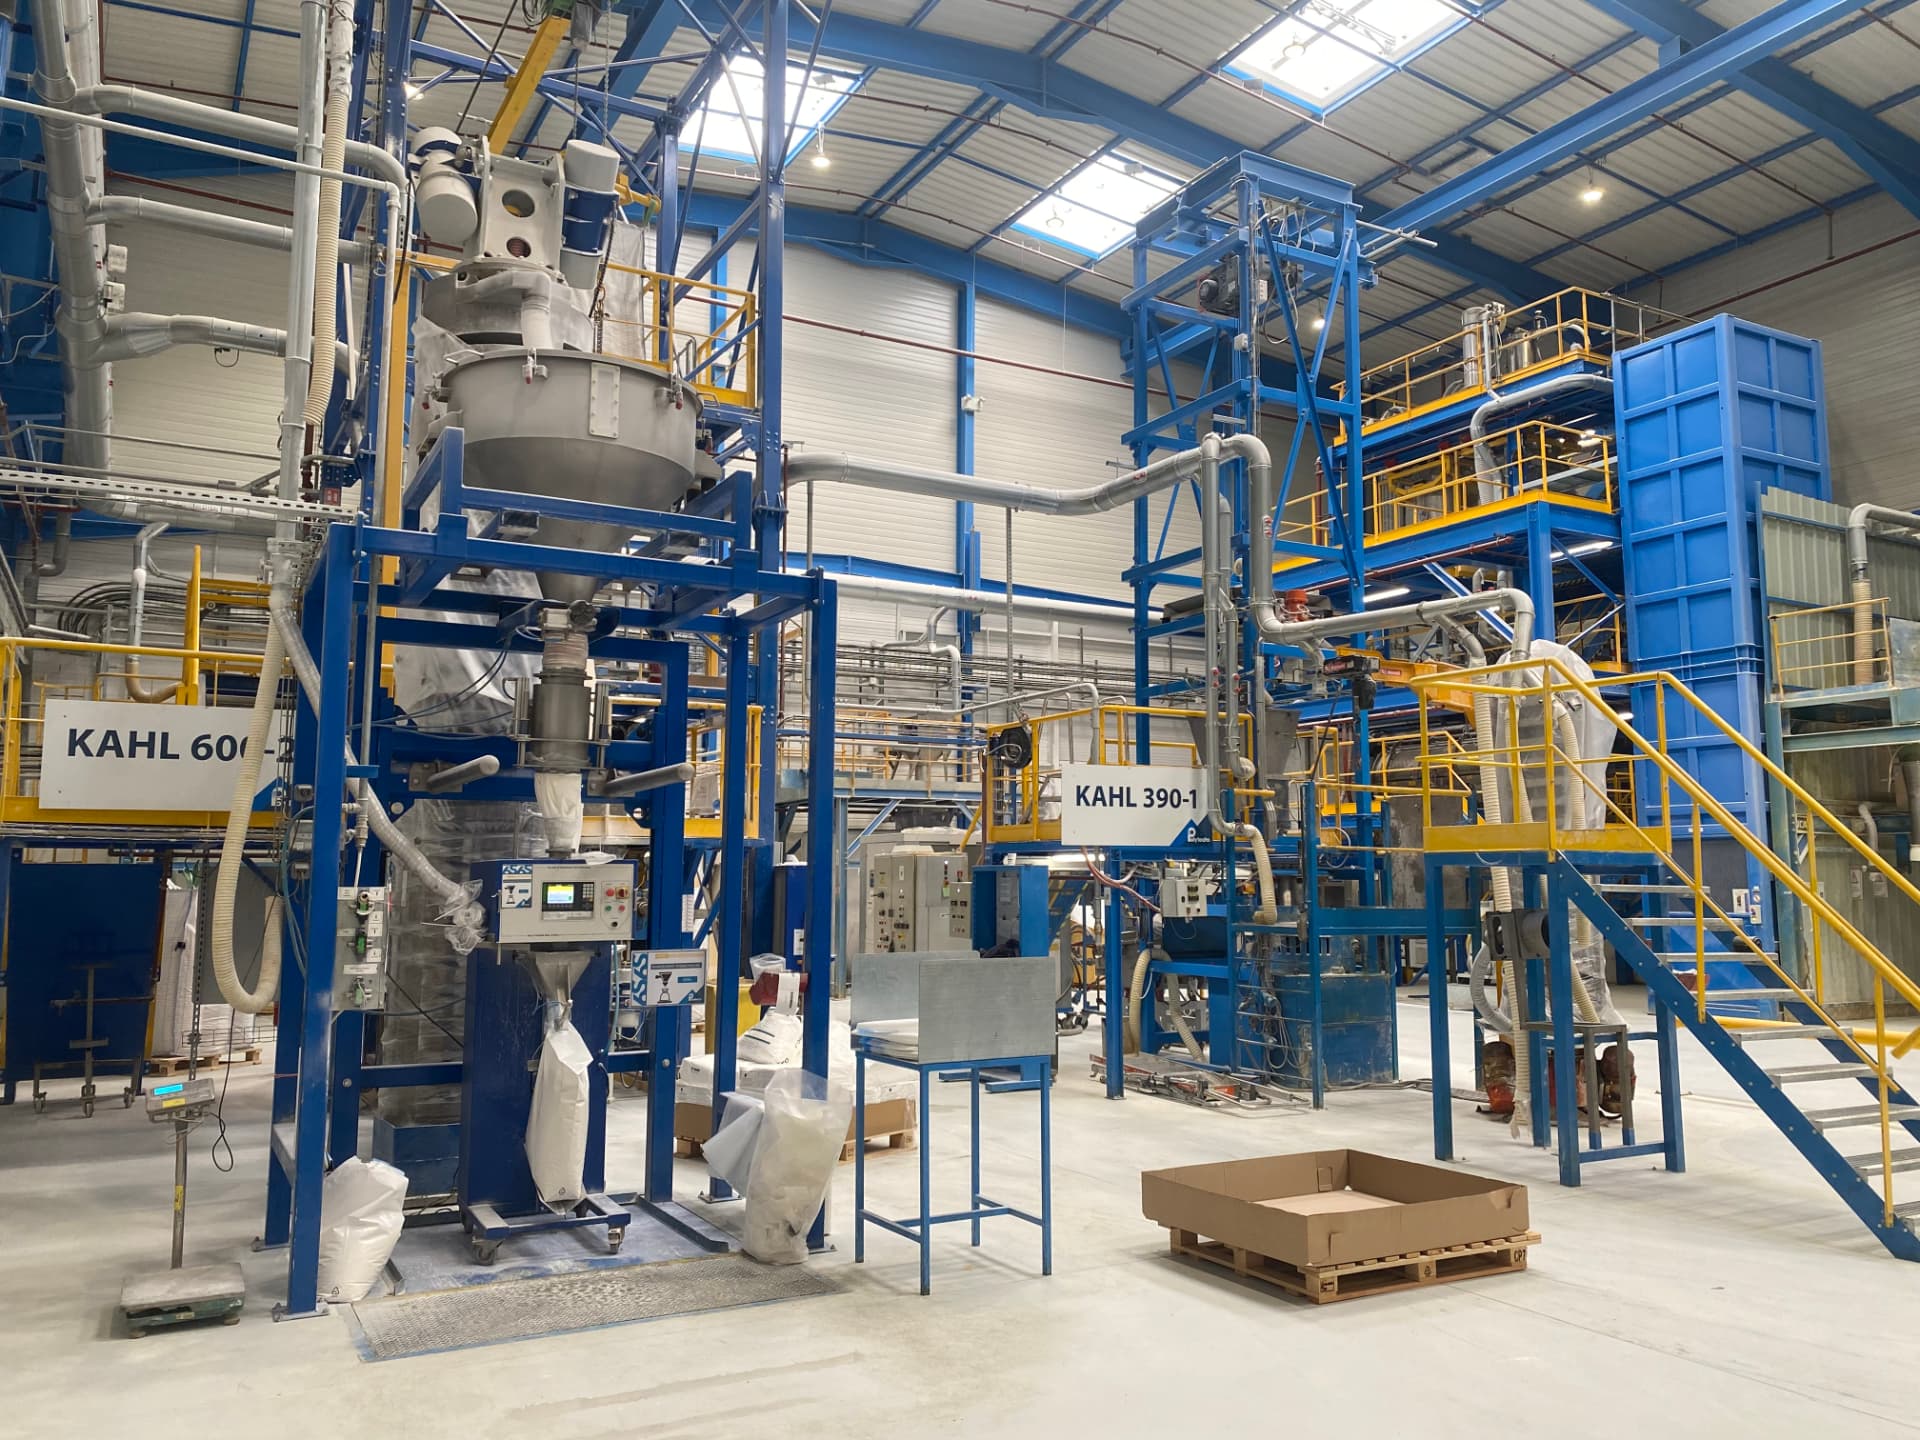
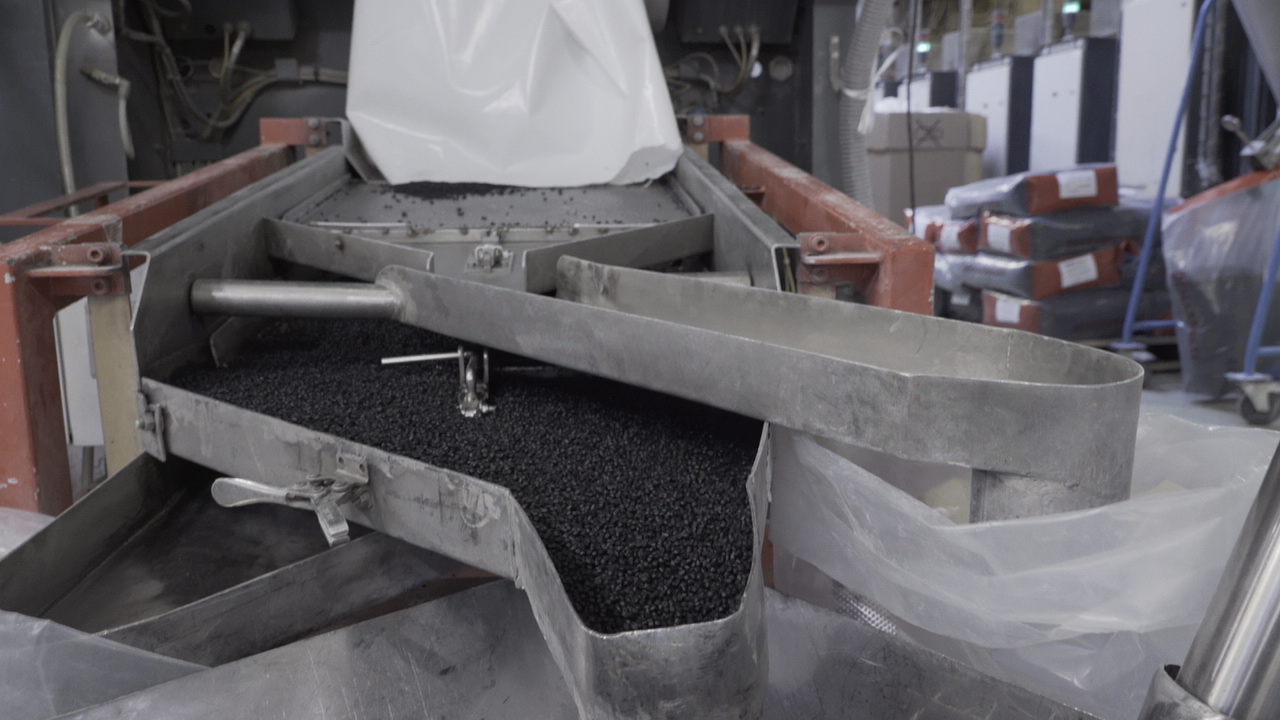
Compaction lines for non-dusting additive blends.
Grafting, peroxide crosslinking and controlled degradation during compounding.
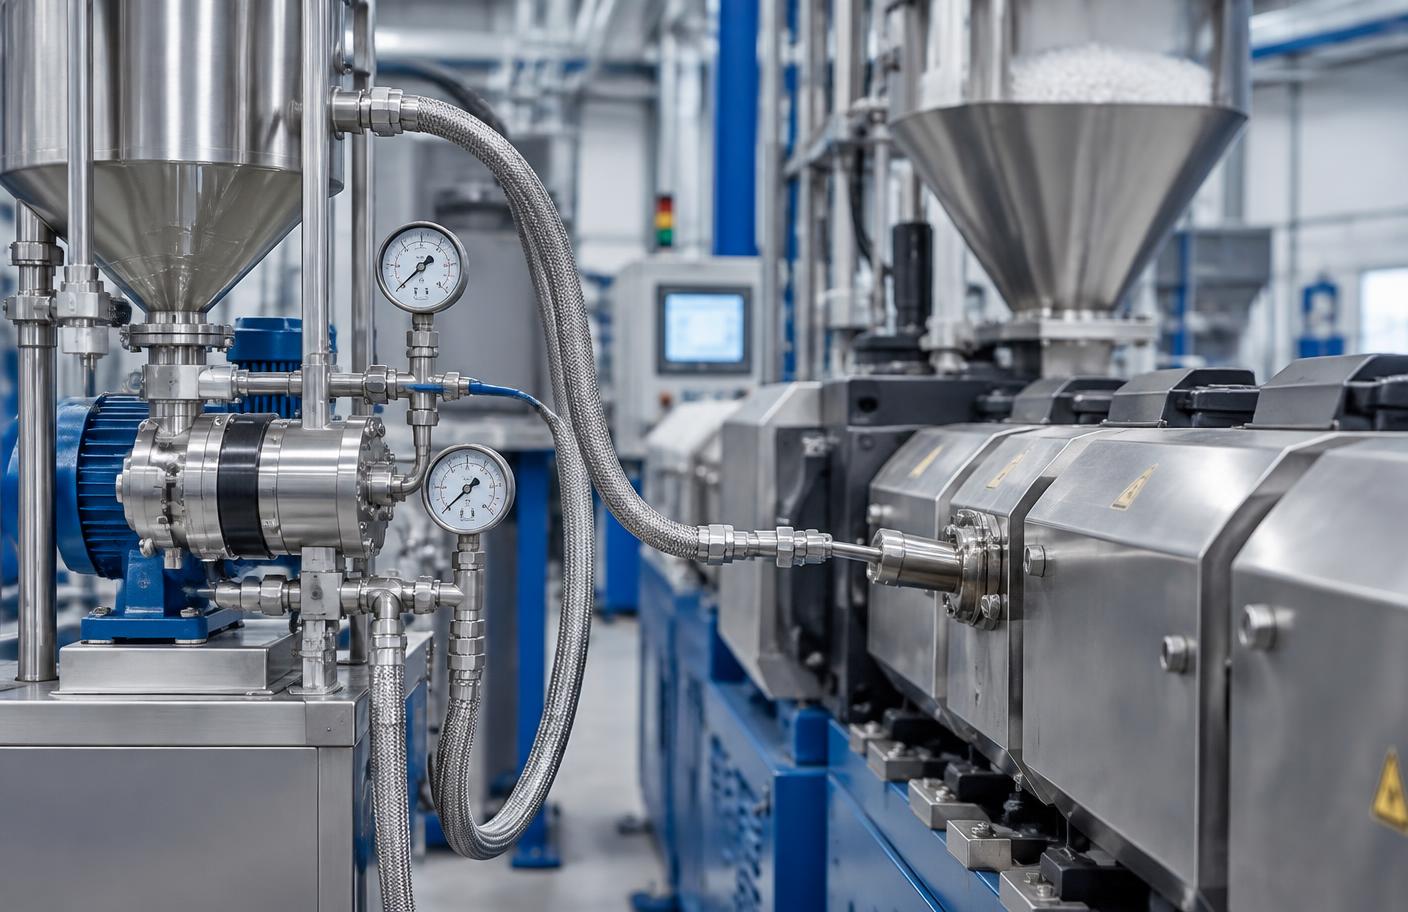
Metered injection of viscous liquid additives into the compounding process.
Stable, dust-free pellets made of 100% additive blends.
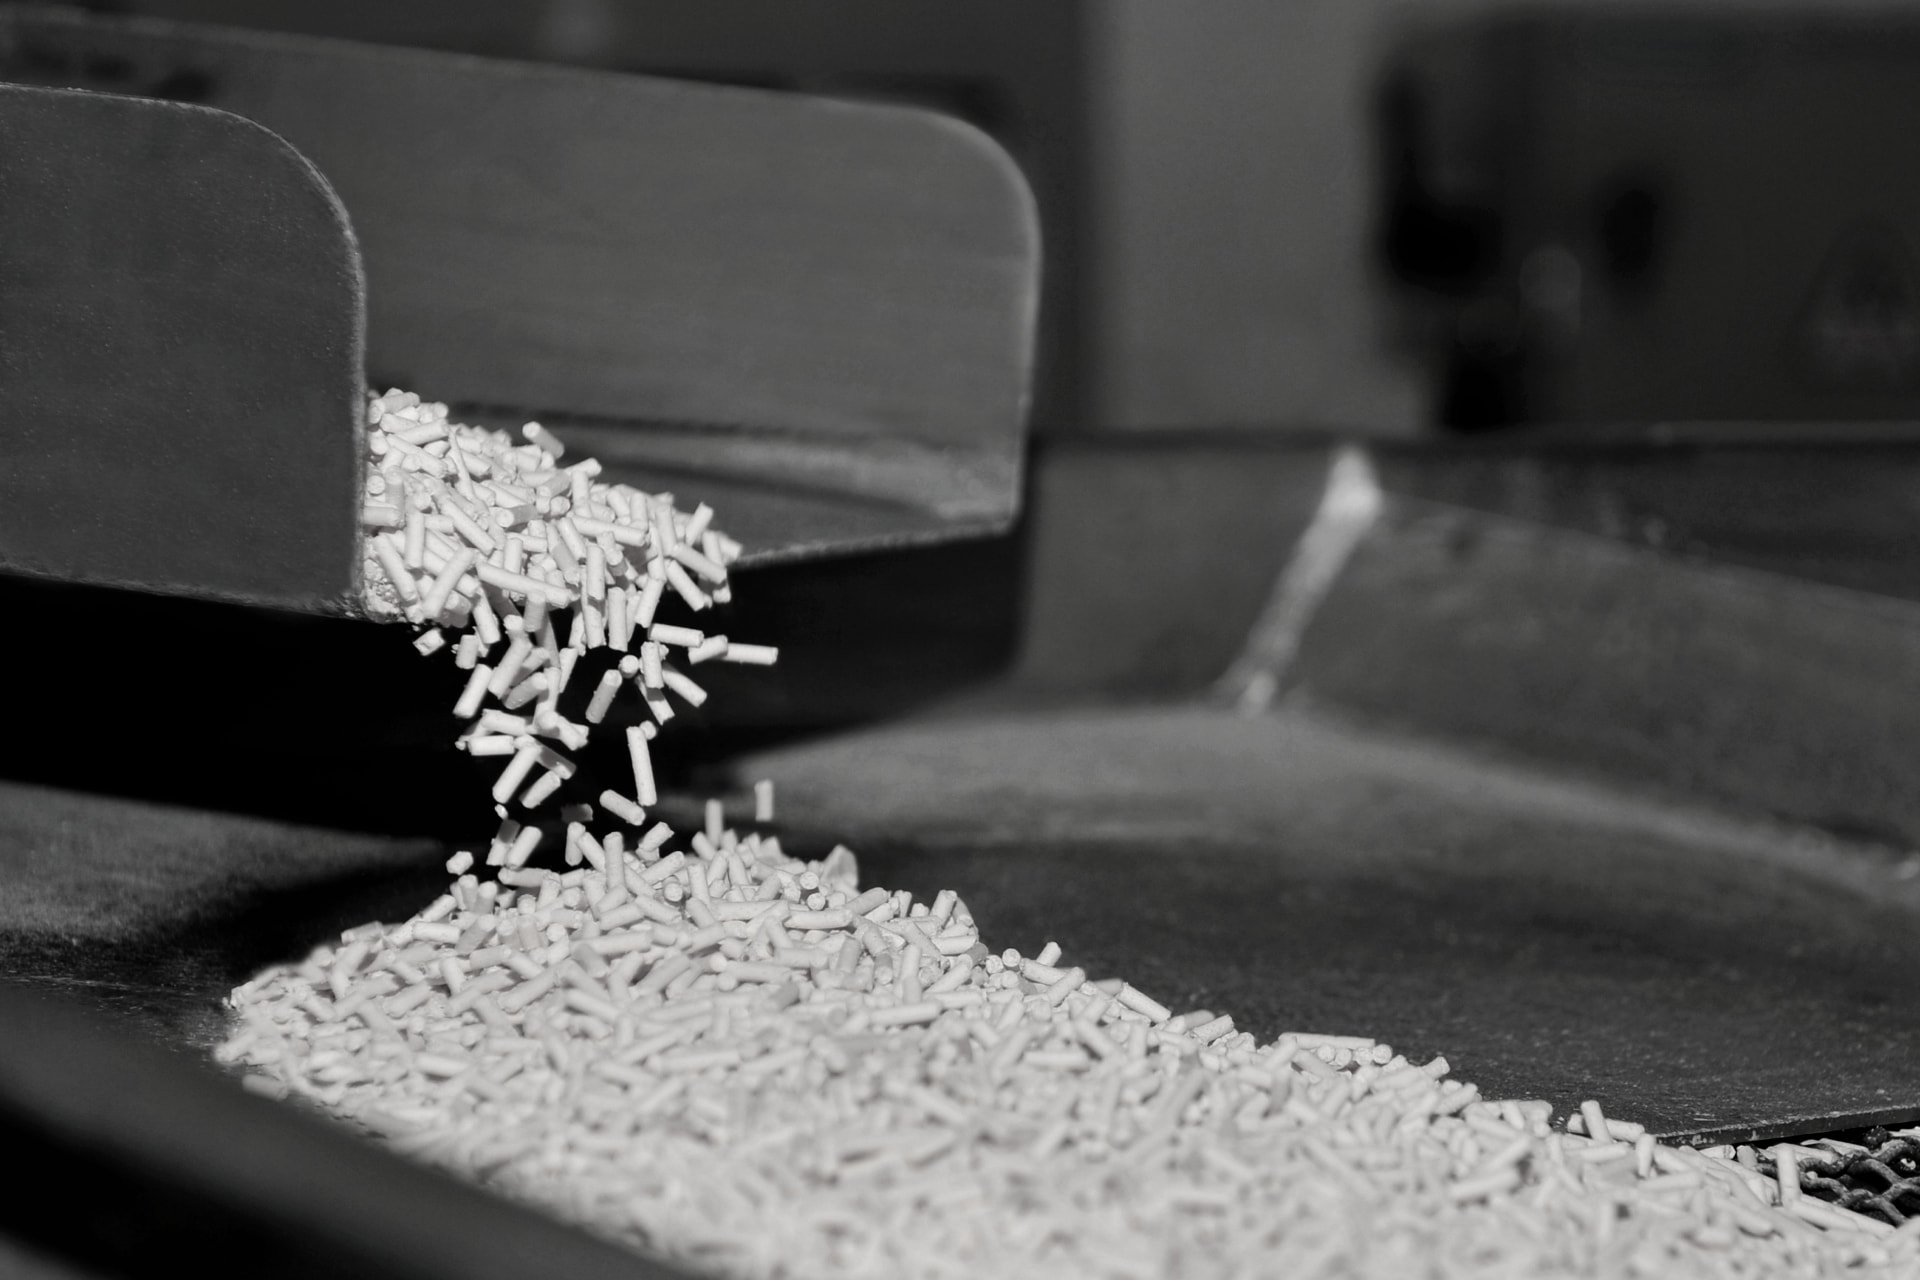
Underwater and air-cut pelletizing, including low-melting-point materials.
If it melts, disperses or grafts, there is a good chance we have run it before. If we haven't, we'll tell you straight away.
Read the chain from left to right. On the left, the raw materials: resins, powders and additives from resin producers, additive suppliers, and bio-based or recycled feedstocks from recyclers. In the centre, Polytechs: the compounding step that turns those inputs into an engineered compound. On the right, the outlets: film converters, cable makers, construction profile extruders, pipe producers and fibre manufacturers.
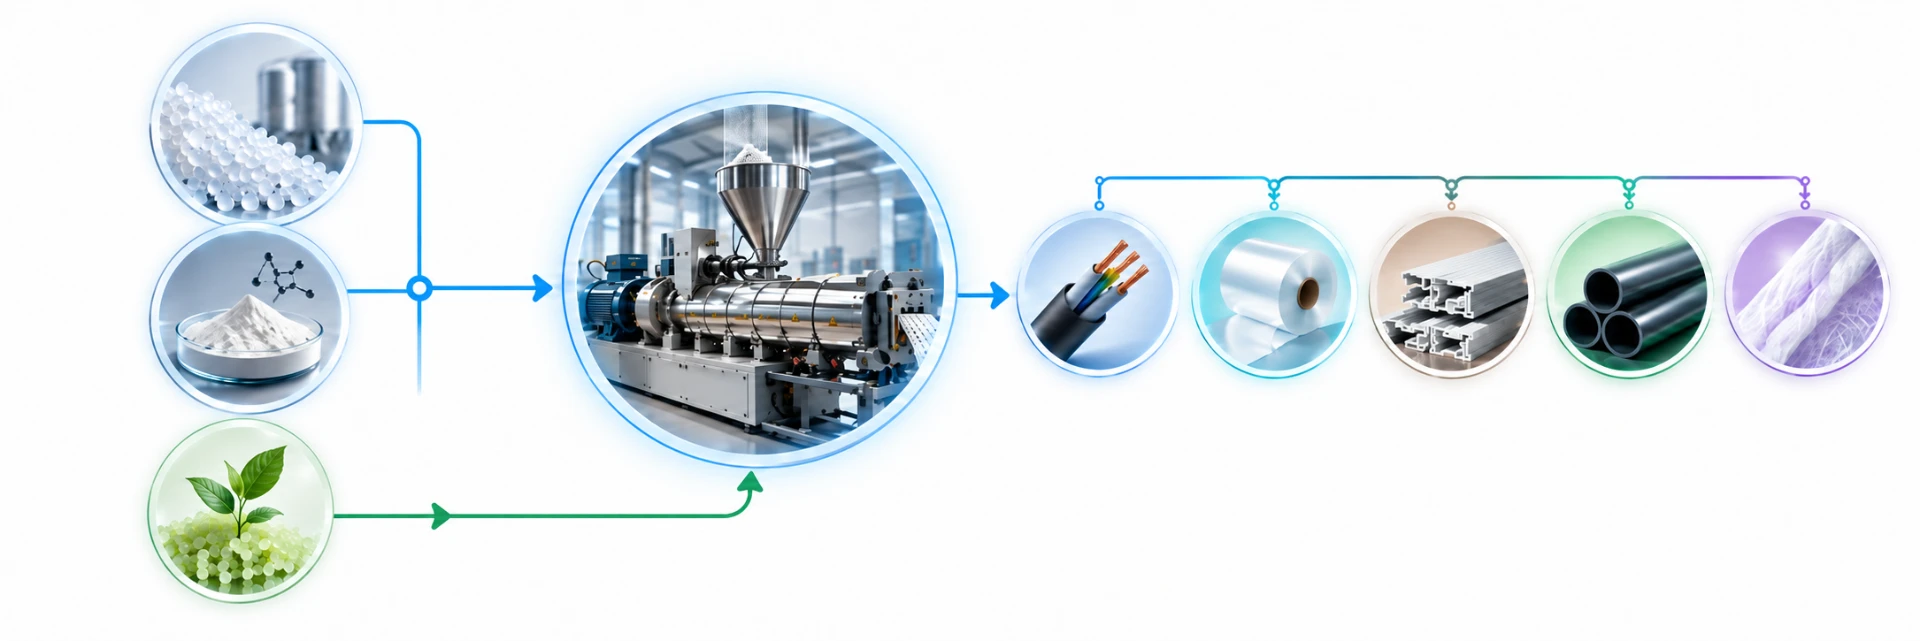
Left · InputsResin producers, additive suppliers and recyclers bring pellets, powders and liquids.
Centre · PolytechsThe compounding step: blending, reacting and pelletizing on our 18+ lines.
Right · OutletsCable, film, construction profiles, pipes and fibre — our partners' end products.
Every project follows five steps, and the NDA always comes first.
From lab batch to mass production on the same line configuration, with the team that will run your campaigns.
Start with the NDA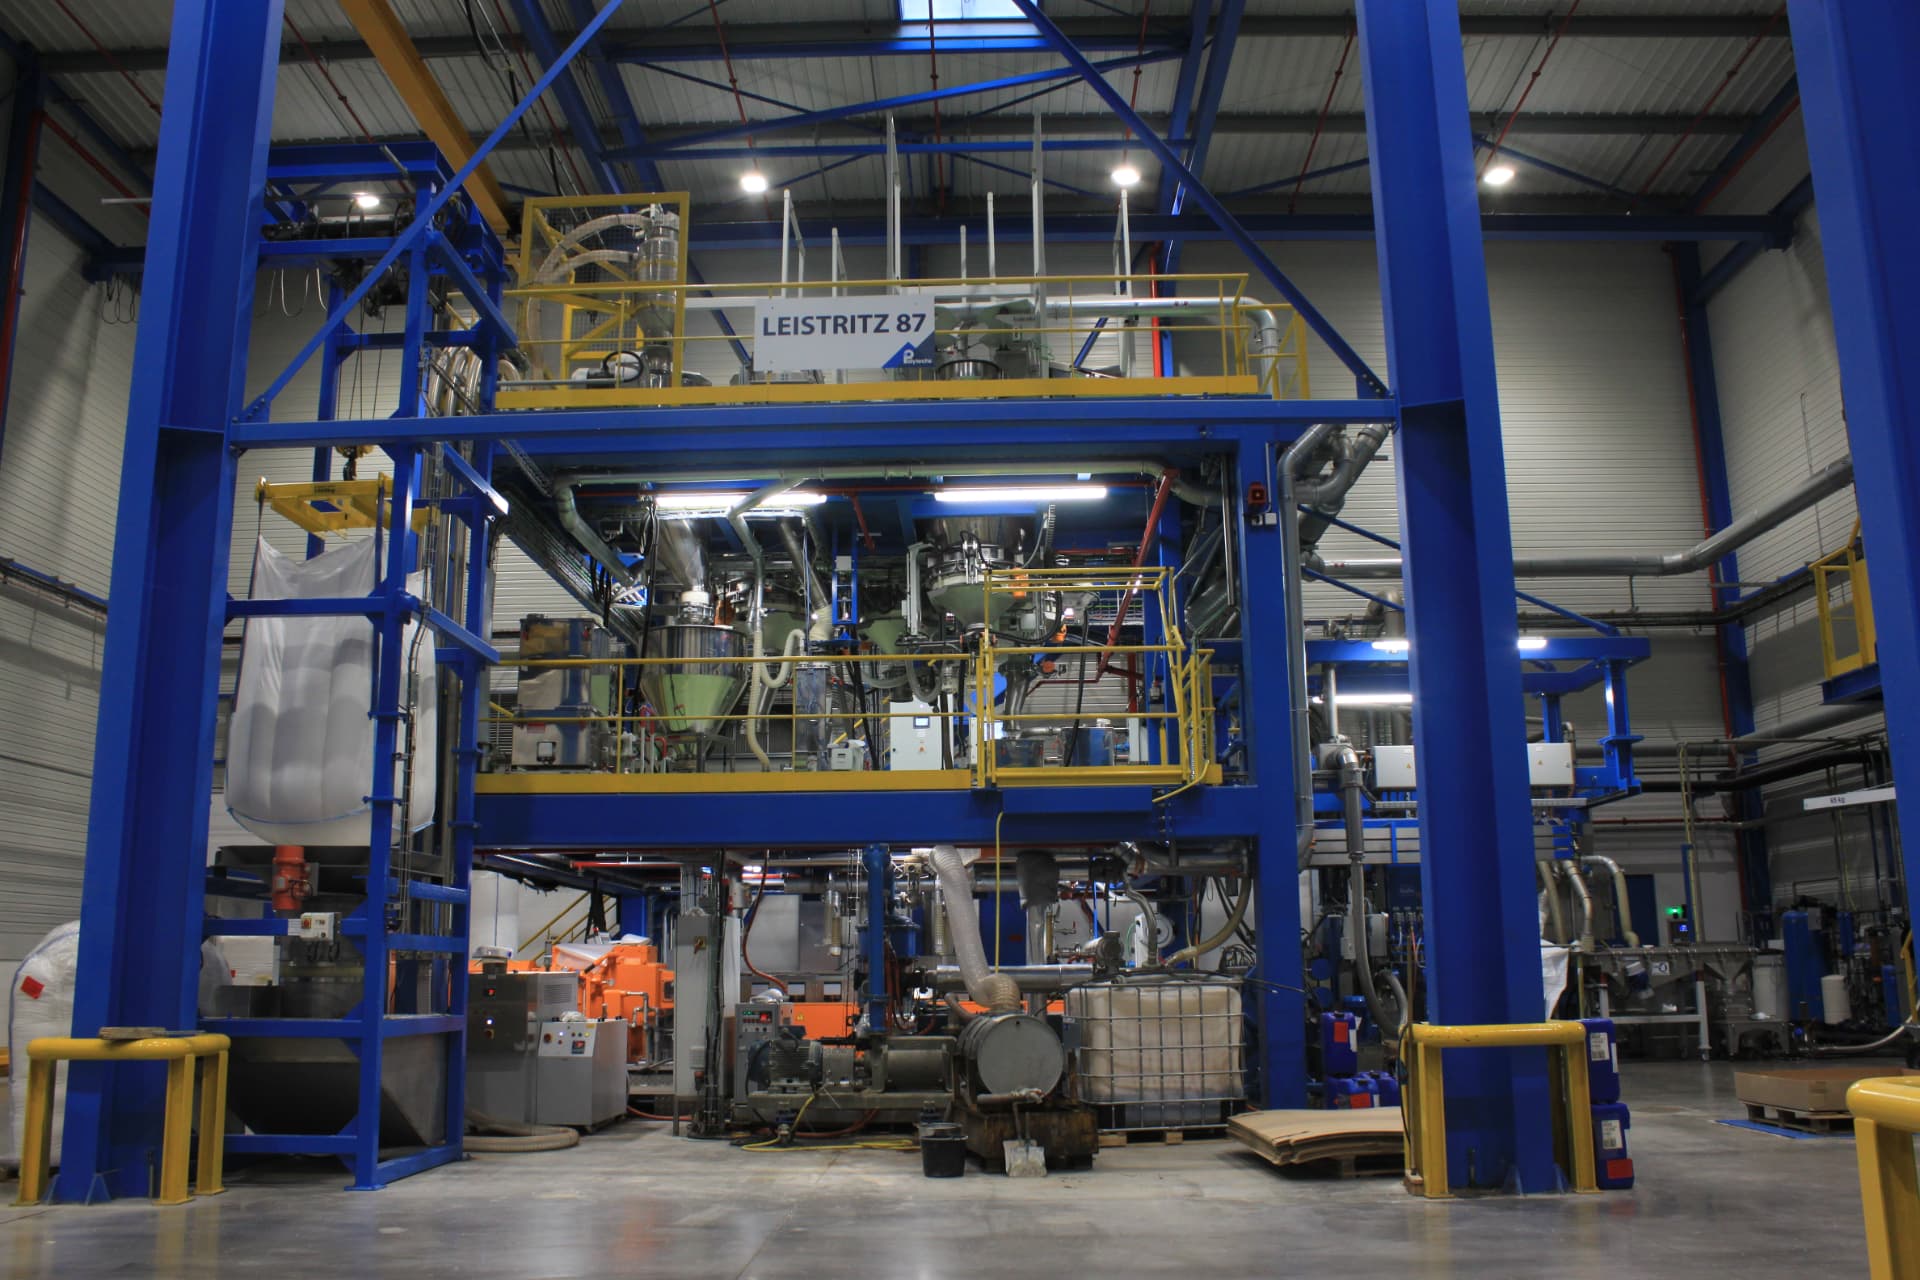
We sign a mutual NDA before you share any recipe or technical data.
Our engineers review your formulation and tell you which line configuration fits it.
We run a first batch and test it in our own lab.
We confirm the process on production-scale equipment against your specification.
We produce your campaigns with the team that ran the trials.
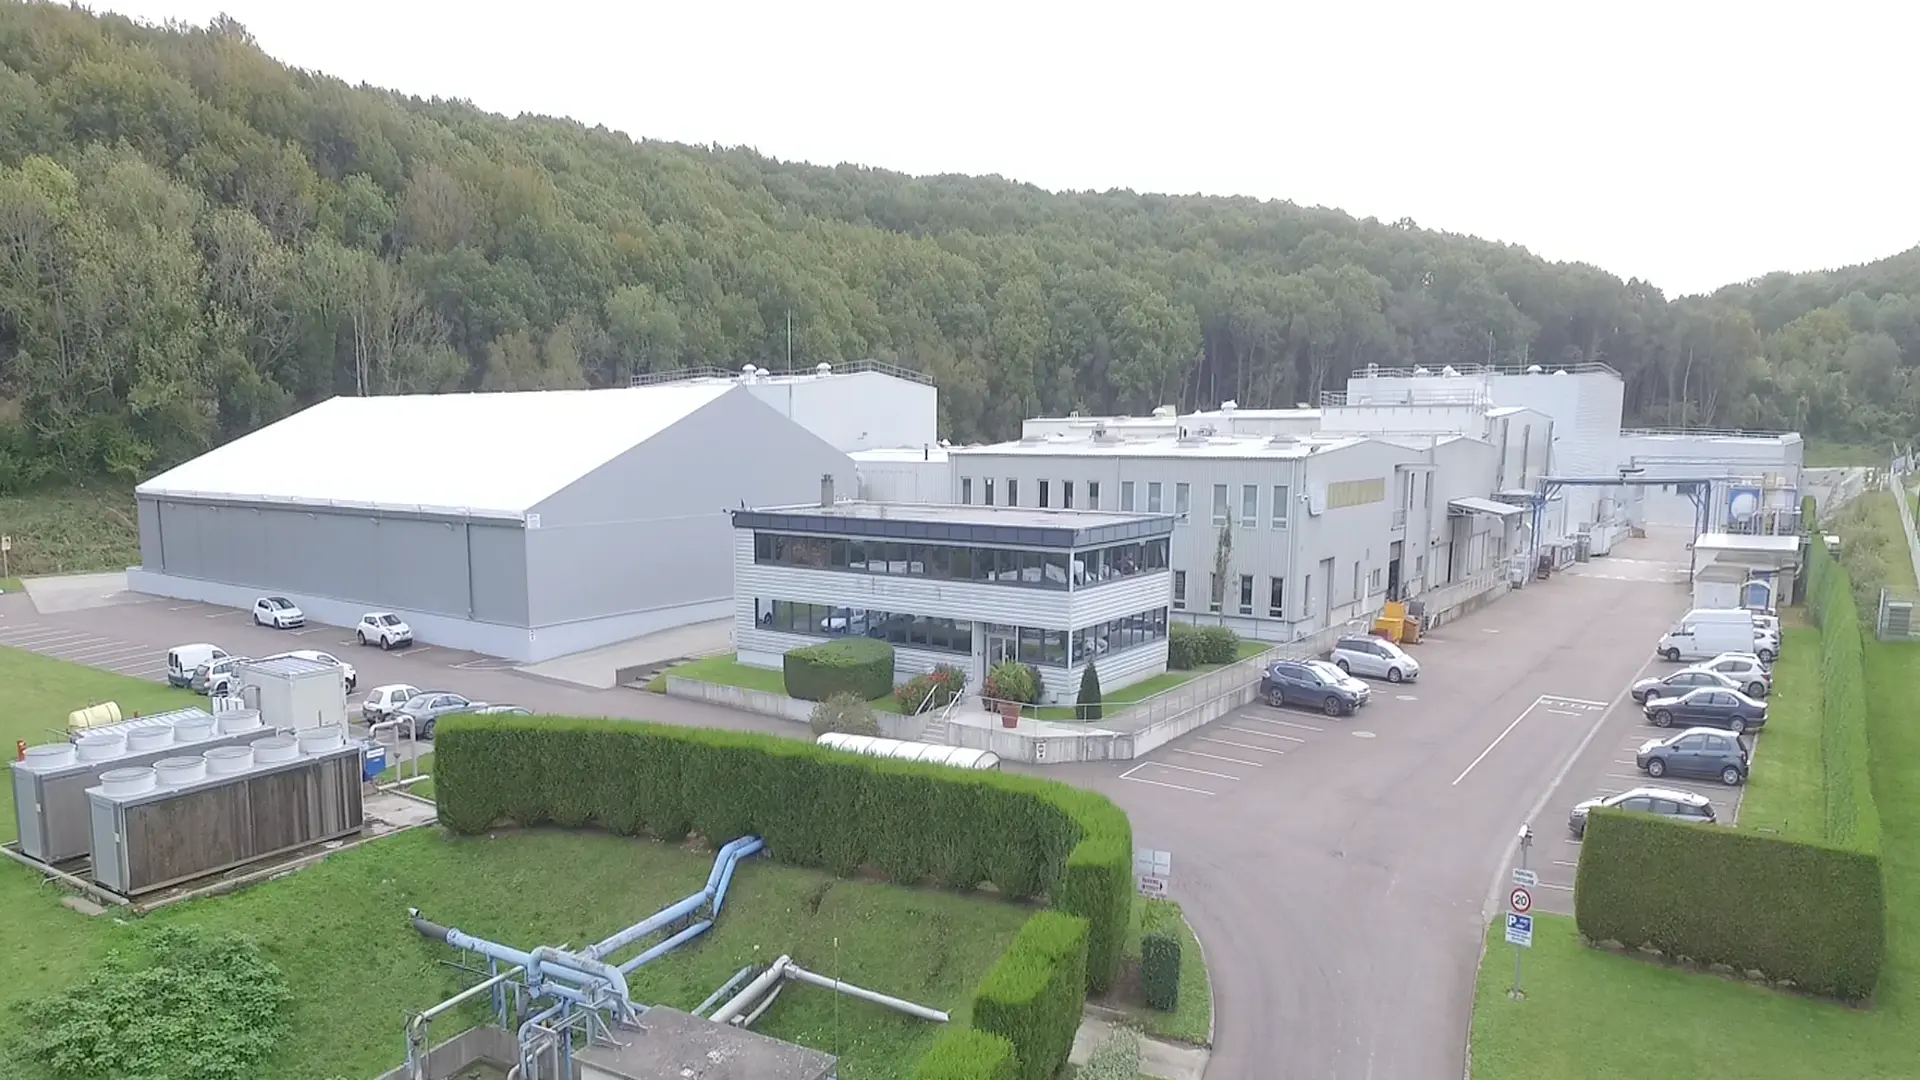
Our own lab checks every lot, and the site is audited against seven schemes.
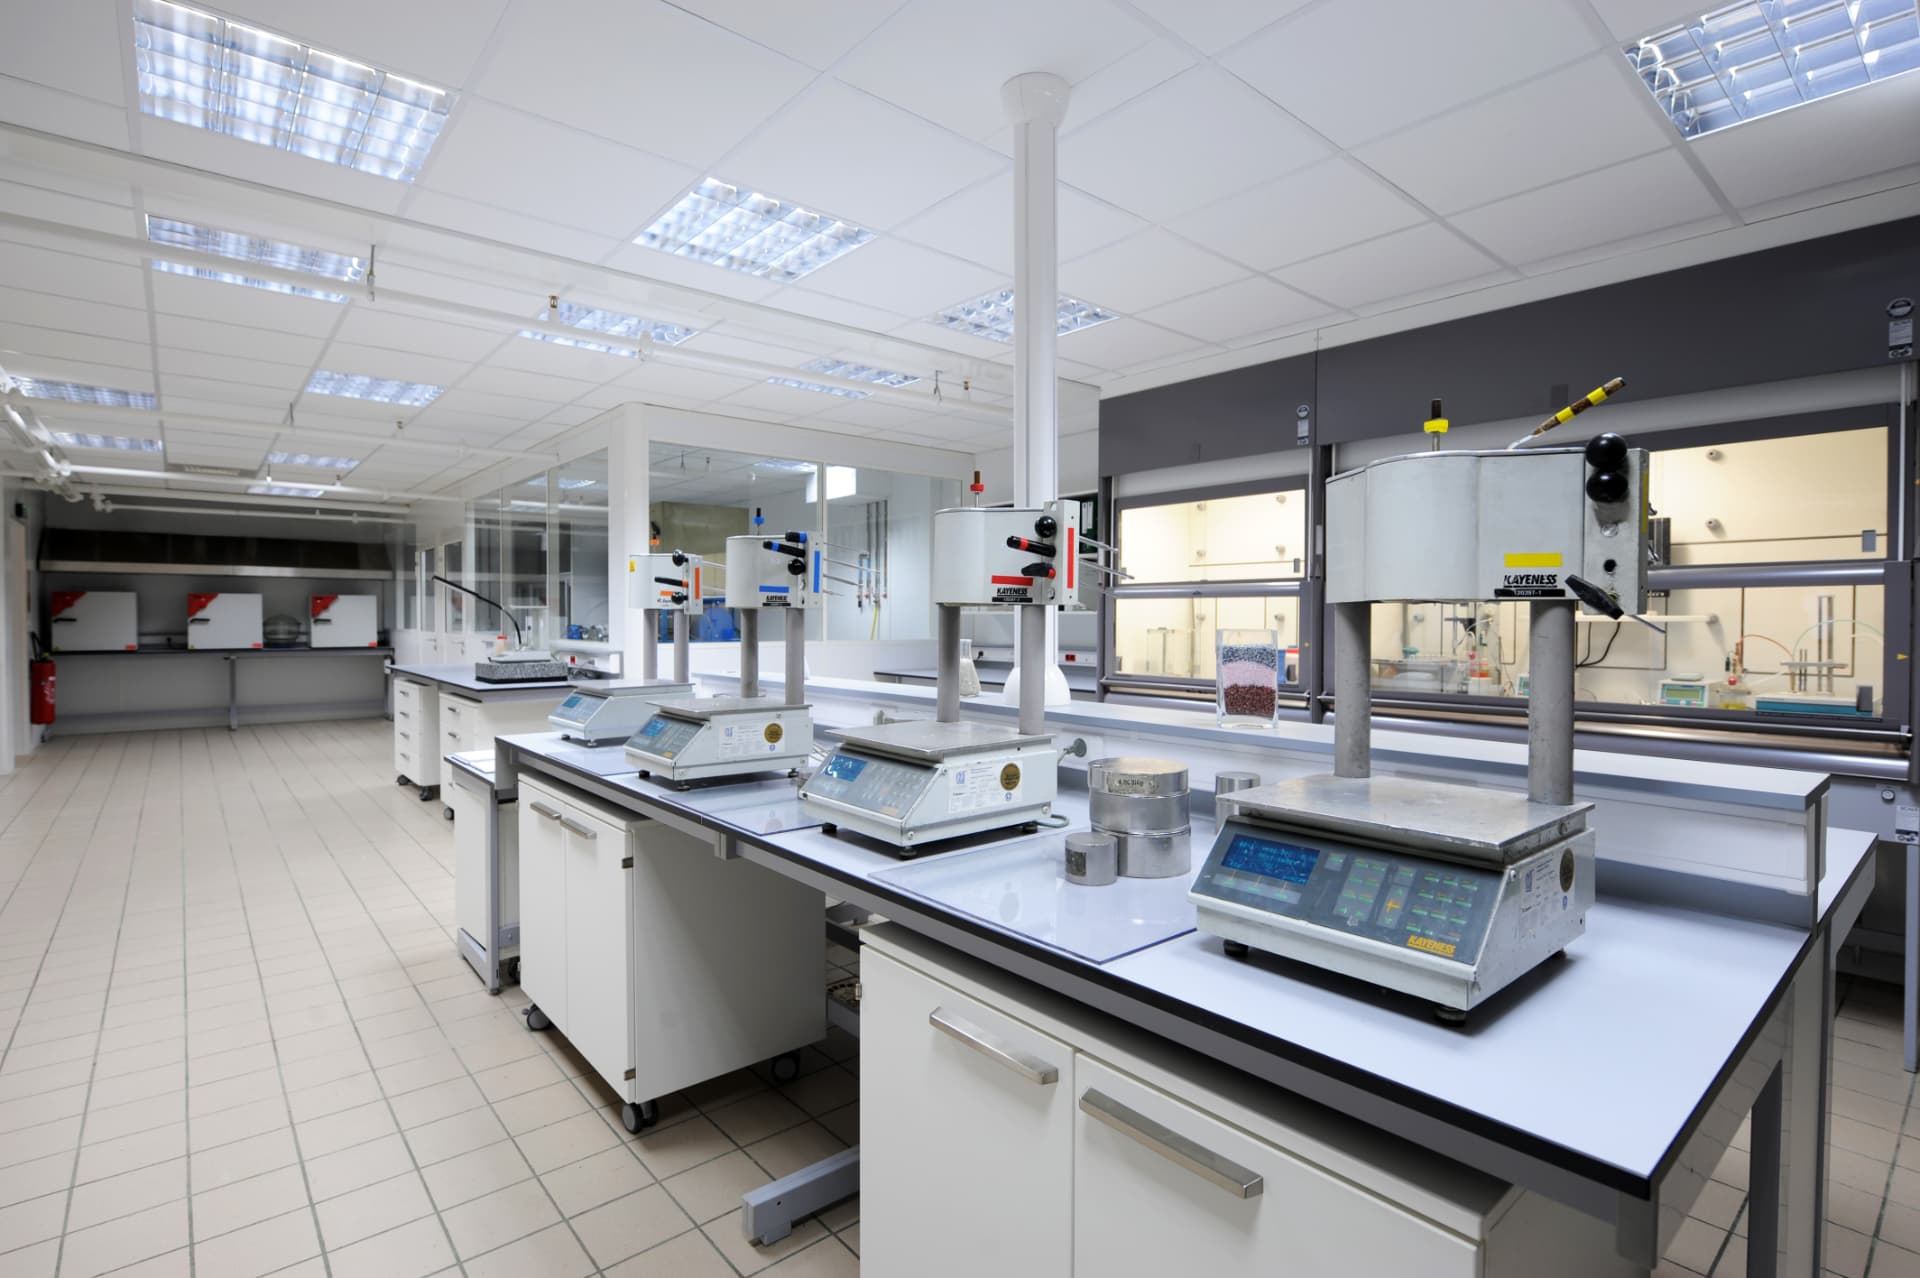
| No. | Test | What it tells you |
|---|---|---|
| 01 | MFI | Melt flow, checked against your specification |
| 02 | Brookfield viscosity | Viscosity of liquid additives and low-melt materials |
| 03 | Density | Filler level and formulation consistency |
| 04 | Ash content | Actual mineral filler loading |
| 05 | Melting point | Thermal behaviour of the compound |
| 06 | Contamination level (film and pellet) | Gels, specks and black spots |
| 07 | Colorimetry | Colour conformity lot to lot |
| 08 | Mechanical properties | Tensile and related properties of the compound |
| 09 | VOC content | Volatile residues after processing |
| 10 | IR spectrometry | Chemical identity of raw materials and compounds |
| 11 | DSC | Melting, crystallisation and curing behaviour |
| 12 | TGA | Thermal stability and composition |
| 13 | HPLC | Additive identification and dosing |
| 14 | Humidity index | Moisture before packing |
ISO 9001
Every campaign follows documented, audited procedures, from raw-material intake to shipment.
ISO 14001
Emissions, waste and energy on the site are managed and audited.
ISO 45001
Safe handling of peroxides and powders is audited, not improvised.
ISCC PLUS
Mass-balance circular and bio-based materials with traceable claims. Claims apply only to materials within the certificate scope.
GPI
Pellet-loss prevention audited on site.
AEO status
Simplified, trusted customs procedures for your imports and exports.
EcoVadis Committed badge
Our CSR performance is assessed by an independent platform.
Toll compounding means we compound your formulation on our lines, to your specification. You keep the recipe and the product IP; we supply the equipment, the process know-how and the team.
Lab trials use the same line configuration as the production campaigns that may follow.
Yes. A bilateral NDA is the first step of every project, before any recipe or technical data is shared. Please do not send confidential recipes before it is signed.
BUSS co-kneaders, co-rotating twin-screw extruders, compaction lines for non-dusting blends, pilot lines, liquid injection, underwater and air-cut pelletizing, across 18+ production lines.
Yes. We can qualify your grade in advance so a second source is ready to produce the same formulation to the same specification if your line stops.
Polyolefins, engineering polymers, fluorinated polymers, epoxy resins, acrylics, rubbers, styrenics, TPEs (TPU, TPE-E, TPV, TPS, TPA), bio-based, biodegradable and recycled polymers.
Last reviewed: